In the modern era of industrial automation, businesses are continuously seeking ways to improve efficiency, reduce operational costs, and enhance safety in remote environments. One technology driving this transformation is the motor operated gate valve — a robust, reliable solution that is redefining fluid control systems across a wide range of industries. As industries evolve, the demand for advanced solutions from gate valve suppliers, butterfly valve suppliers, and valve manufacturers continues to grow, supported by the availability of ex stock valves and the expanding role of Valve Stockist in UAE and beyond.
The Intersection of Automation and Industrial Fluid Control
Traditionally, gate valves have been manually operated, requiring personnel on site to physically open or close valves. While this approach worked in contained environments, it poses significant challenges in remote or hazardous locations such as oil fields, offshore platforms, chemical plants, and large water networks.
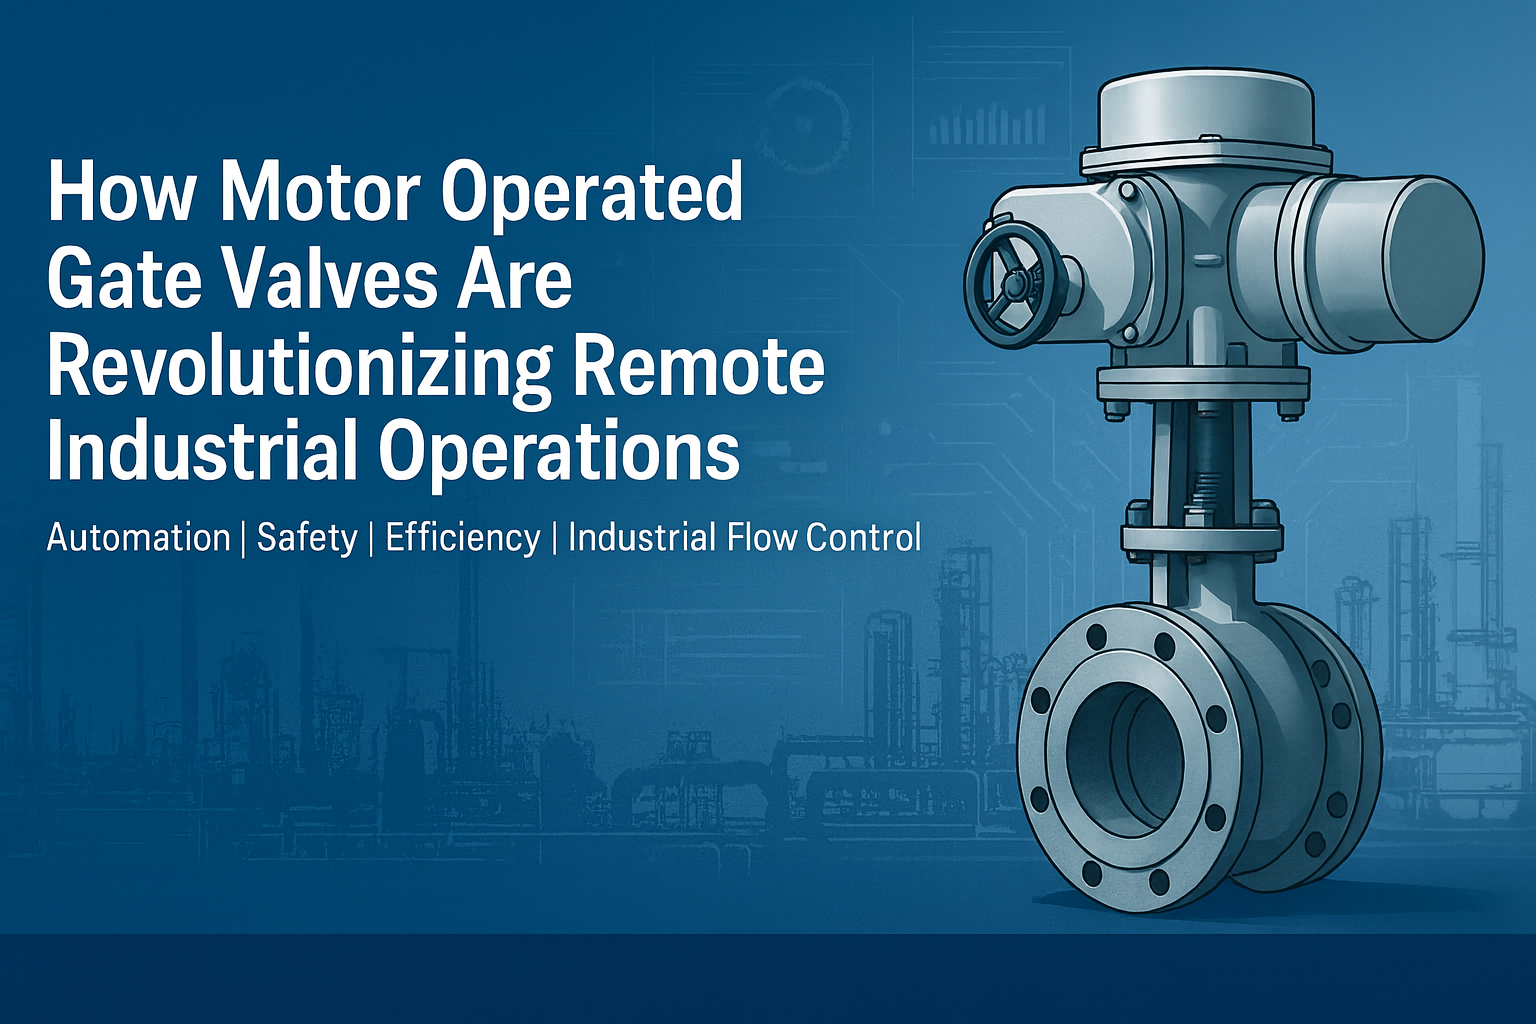
With the advent of motor operated gate valves, industries have gained the ability to automate flow control, allowing operations to be managed remotely with precision and safety. These valves incorporate an electromechanical actuator — often a geared motor — that controls the valve’s movement based on real-time inputs from control systems like PLCs (Programmable Logic Controllers) or SCADA (Supervisory Control and Data Acquisition).
Why Motor Operated Gate Valves Are a Game Changer
- Enhanced Remote Control and Monitoring
One of the most compelling advantages of motor operated gate valves is the ability to control operations from distant command centers. Remote actuation removes the need for personnel to travel to remote sites for manual adjustments. This not only saves time and cost but also mitigates human exposure to hazardous environments.
In emergency situations, such as leaks or rapid pressure changes, motor operated gate valves can be instantly actuated to isolate sections of a plant — a capability not feasible with manual valves.
- Precision and Reliability
Motor operated gate valves provide precise control over fluid flow. The integration of position feedback systems enables exact monitoring of valve status — open, closed, or part-open — allowing tighter control of processes. This precision is crucial in industries like petrochemicals, where even minor deviations in flow can impact product quality and safety.
Top valve manufacturers design these automated gate valves to withstand harsh industrial conditions, ensuring high reliability and longer service life even under extreme temperatures and pressures.
- Seamless Integration with Automation Systems
In the age of Industry 4.0, connectivity and data integration are paramount. Motor operated gate valves easily connect with digital control systems, offering real-time data communication between field devices and centralized systems. This interoperability is crucial for predictive maintenance, efficiency optimization, and full plant automation.
Whether integrated into an existing SCADA system or a fully digitized automation platform, these valves allow operators to gather actionable insights that improve overall performance.
- Better Safety and Compliance
Industrial environments carry inherent risks — from flammable fluids to toxic gases. Reducing human intervention in such settings enhances safety. With motor operated gate valves, hazardous tasks such as emergency shut-offs can be executed remotely, supporting compliance with safety standards and regulations.
Additionally, these valves are often paired with safety interlocks and automated alerts — features that butterfly valve suppliers and gate valve suppliers emphasize to meet strict industry requirements.
Comparing Motor Operated Gate Valves with Other Valve Types
While motor operated gate valves are highly effective for full flow or shut-off applications, industries often use a variety of valves depending on process needs. For example:
- Butterfly valves— typically supplied by butterfly valve suppliers — are ideal for applications requiring fast cycling and moderate throttling. They are lighter and more cost-effective but may not handle high pressures as well as gate valves.
- Globe valves— better suited for throttling and precise flow control, but more complex and expensive in larger sizes compared to gate valves.
Despite these differences, gate valves — particularly when motorised — remain the preferred choice for on/off service applications where tight sealing and minimal flow restriction are priorities.
The Importance of Stock Availability: Ex Stock Valves & Valve Stockists
In fast-moving industrial sectors, downtime is costly. One key way businesses are reducing lead times and ensuring operational continuity is by sourcing ex stock valves — pre-manufactured valves ready for immediate dispatch.
A reliable Valve Stockist in UAE plays a pivotal role here, offering a selection of motor operated gate valves, butterfly valves, and other industrial valves from reputable valve manufacturers. This stock availability allows companies to rapidly replace faulty components, expedite project timelines, and reduce inventory costs without compromising quality.
Valve stockists often maintain an extensive range of valve sizes, materials, and actuation options — a critical advantage for industries with varied fluid control needs. By partnering with reputable suppliers, businesses gain access to certified products that meet international standards, further ensuring longevity and performance.
Real-World Impact Across Industries
Motor operated gate valves are increasingly used across sectors including:
- Oil & Gas: Automating flow control in pipelines, tank farms, and offshore platforms to improve safety and environmental compliance.
- Water Treatment: Managing large-scale distribution and wastewater processes with precision and minimal manual intervention.
- Power Generation: Supporting cooling systems, boiler feed lines, and steam control with high reliability.
- Chemical Processing: Enabling remote flow isolation in corrosive and high-temperature environments.
In each case, the transition from manual to motor operated gate valves has enabled companies to increase uptime, reduce operational costs, and safeguard personnel.
Conclusion: A Smart Move Toward Industrial Automation
As remote operations become the new norm for industrial facilities worldwide, motor operated gate valves are rapidly emerging as indispensable components in advanced fluid control systems. Their ability to enhance safety, boost efficiency, and integrate seamlessly with automation platforms positions them as essential assets for forward-looking businesses.
Whether you’re sourcing from trusted gate valve suppliers, comparing options from butterfly valve suppliers, or leveraging the convenience of ex stock valves through a reputable Valve Stockist in UAE, investing in motorised valves is a strategic step toward smarter, more resilient industrial operations.